ISO 9001 · ISO 14001 · ISO 45001 · CE · UDEM · EAC · CQC
🇸🇦 Saudi Arabia · Solar
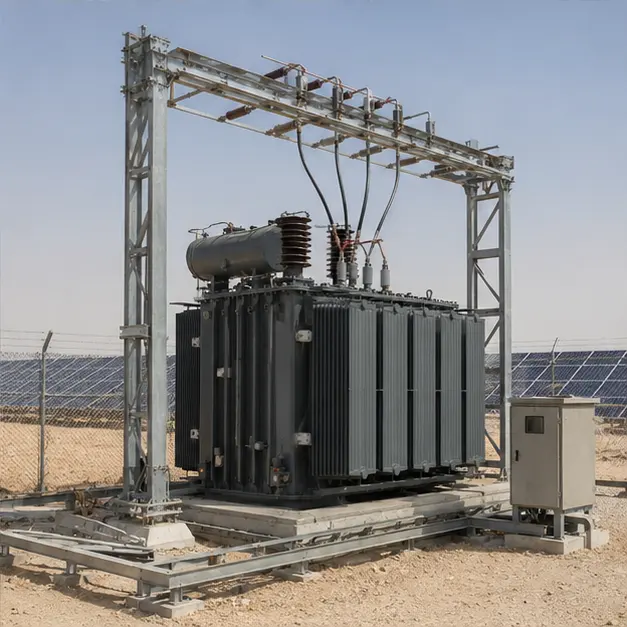
Saudi Arabia: 33 kV/13.8 kV Solar Transformer Bay
Reference configuration: 33 kV/13.8 kV oil-immersed power transformer bay for utility-scale photovoltaic power station in Saudi Arabia — 33 kV / 13.8 kV, 60…
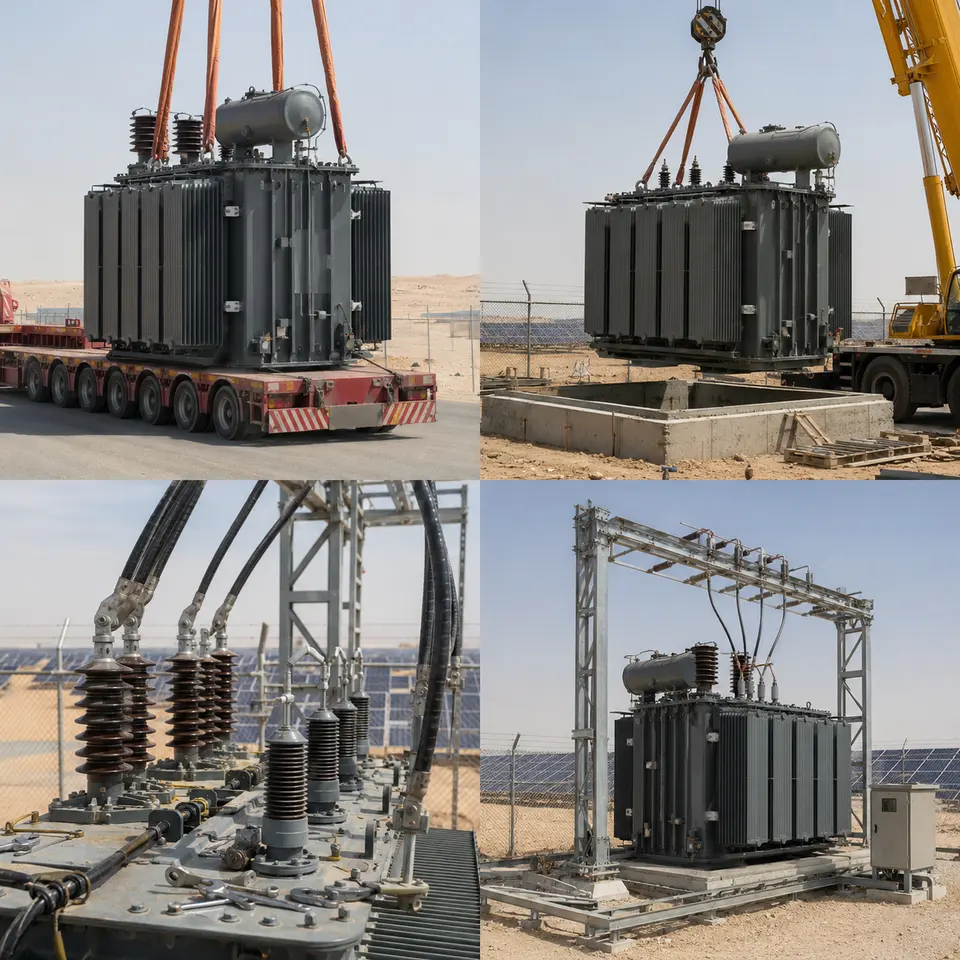
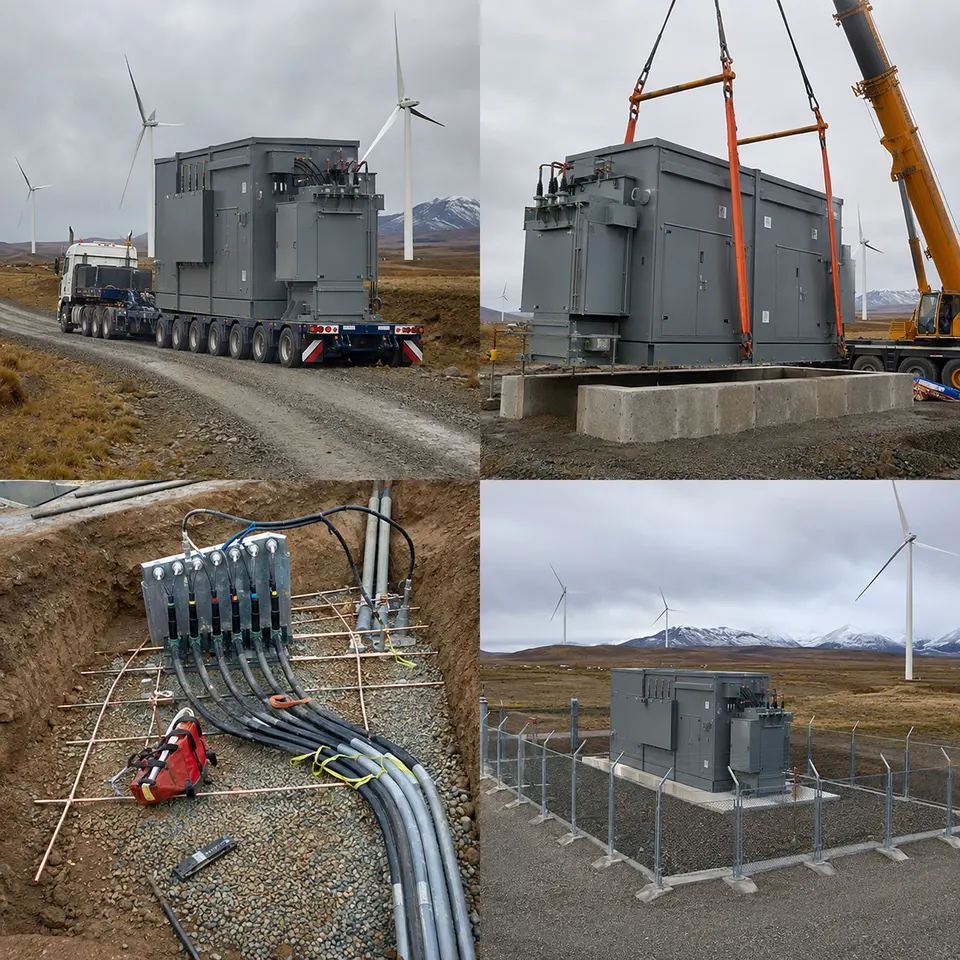
Four-stage sequence for an oil-immersed transformer bay of the type used at utility-scale PV plants in Saudi Arabia
Representative project visualisation. The images in this set are representative visualisations illustrating a typical configuration of this equipment type. They are not photographs or documentary evidence of a delivered project, and they do not represent a specific customer, site, contract, commissioning date or third-party approval. Ratings, quantities and arrangements shown are illustrative and would be fixed against a real enquiry.
At a glance
Country
Saudi Arabia
Application
Utility-scale photovoltaic power station
System
33 kV/13.8 kV oil-immersed power transformer bay
Voltage
33 kV / 13.8 kV
Frequency
60 Hz
Standards basis
IEC 60076-1/-2/-3/-5/-7 (transformer, temperature rise, insulation, short circuit, loading), IEC 60137 (bushings), IEC 60099-4 (surge arresters), IEC 61936-1 (AC installations above 1 kV), IEC 60815 (creepage for polluted conditions)
A transformer bay serving a Saudi photovoltaic plant has to cope with three conditions that a standard distribution unit was never designed around.
Ambient temperature comes first. Because IEC 60076-2 defines temperature rise above ambient, a site with consistently high daytime air temperature has already eaten into the hot-spot margin before a single watt of load is applied. Rating, oil and winding rise limits, and radiator surface area all need to be set against the site's actual design ambient rather than the standard's reference values.
The load shape comes second. A PV plant generates nothing at night, climbs through the morning and can run near full output for hours at a stretch — a cyclic duty that calls for the IEC 60076-7 loading guide and the design's real thermal time constants, rather than treating it as a flat, continuous rated load. There's also harmonic content from the inverters to account for, which pushes eddy and stray losses higher than the sinusoidal case would suggest and raises the hot-spot temperature for a given rms current.
The environment is the third factor. Airborne dust and sand foul insulator and bushing surfaces, so creepage distance has to be chosen for a heavy pollution class, and the radiator fins and cooler intakes need to stay accessible for cleaning. UV exposure and thermal cycling wear down gaskets and paint over time, which means coating class and gasket material belong in the electrical specification rather than being treated as an afterthought.
Running at 60 Hz instead of 50 Hz isn't a trivial swap either: core flux density drops for the same applied voltage and turns count, eddy-current and stray losses climb with frequency, and reactance scales up as well. A unit meant for this duty is designed for 60 Hz from the start rather than adapted from a 50 Hz base.
System configuration
Item
Description
Specification notes
Power transformer
Oil-immersed 33 kV/13.8 kV step-up unit for PV export
Rating, impedance and vector group set by the plant's inverter block layout and the grid connection study
Cooling
Radiator bank, ONAN or ONAF with fan control
Radiator surface and fan staging sized on the site design ambient and the daily PV load cycle, not on standard reference ambient
Oil preservation
Conservator with air dryer or sealed system
Conservator volume covers the oil expansion range across the full day-to-night temperature swing
Bushings and terminations
HV and MV bushings with connection to the station gantry
Creepage class selected for heavy pollution; connectors sized for both current and mechanical load from conductor and wind
Surge protection
Arresters on the HV and MV sides
Rated and continuous operating voltage selected against the system earthing arrangement and expected temporary overvoltage
Protection and monitoring
Buchholz relay, oil and winding temperature indication, pressure relief, oil level, differential and overcurrent protection
Contacts wired to the plant protection and SCADA; winding temperature used for fan control and alarm
Earthing
Station earth grid, tank and neutral earthing, gantry bonding
Conductor sized for prospective fault current and clearing time; step and touch potential verified for the bay layout
Foundation and containment
Reinforced plinth, rails or pads, oil containment and drainage
Containment volume matched to the oil quantity and local environmental requirement
Enclosure and finish
Outdoor construction, coating and hardware
Coating class and gasket material selected for UV, sand abrasion and wide diurnal temperature swing
Installation sequence
Overview — Four-stage sequence for an oil-immersed transformer bay of the type used at utility-scale PV plants in Saudi Arabia
The contact sheet walks through the four stages that a bay installation of this type goes through: transport and delivery, crane placement, high-voltage termination work, and the finished bay. Physical dependency fixes this order in place. The foundation, earth grid and oil containment all need to be finished and proved before the transformer arrives, since large parts of them end up buried under the tank afterward. Radiators, conservator and bushings go on after the unit is set down, which keeps the transport mass and profile inside road limits during the journey. Terminations come next because their geometry depends on exactly where the transformer ends up sitting. Testing closes out the sequence, ahead of the bay being fenced and cleared for energisation.
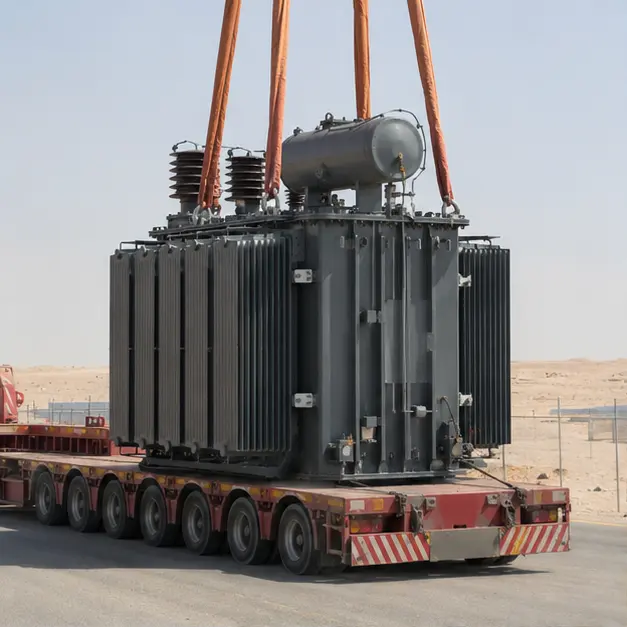
Delivery — Heavy transport of an oil-immersed power transformer of this type to a photovoltaic site
A transformer of this size doesn't travel fully assembled — radiators, conservator and sometimes even the bushings ship separately, and the tank itself may travel under dry-air or nitrogen pressure rather than filled with oil. So delivery checks focus on transport integrity rather than final assembly: impact recorders are read against the agreed shock limits, gas pressure is confirmed positive, and gasketed joints and blanking plates are checked for any sign of leakage. The route in matters as much as the load itself — axle loading, bridge capacity, overhead clearance and turning radii on desert site roads all get assessed before the vehicle sets out, not once it arrives.
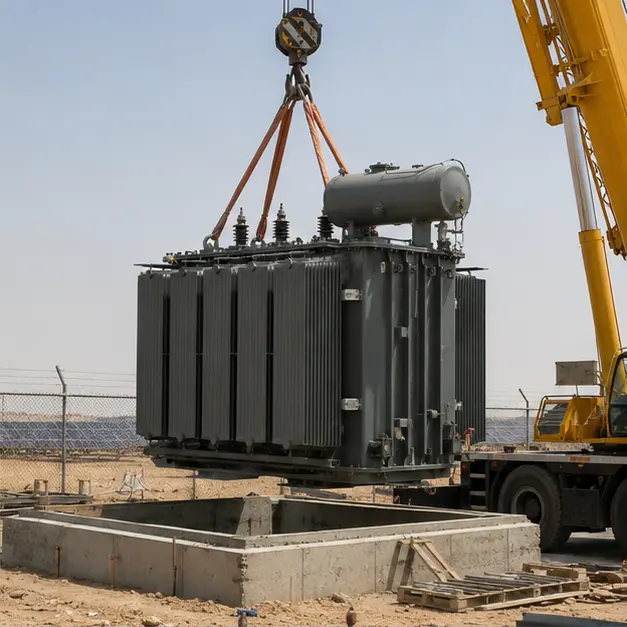
Placement — Crane placement of the transformer onto its prepared foundation in an arrangement of this type
Placement is the lift that governs the whole operation. Rigging goes through the manufacturer's designated lugs, with the sling geometry set so the resultant force runs through the actual centre of gravity — a transformer's mass concentrates at the core and windings, which rarely line up with the tank's geometric centre. Crane capacity is checked at the working radius, on ground whose bearing pressure has been verified under the outriggers, and wind speed is tracked throughout because a large tank presents a lot of sail area. The plinth is levelled before the unit touches down; setting it out of level distorts gasket compression at the cover and radiator flanges and throws off the oil-level gauge reading.
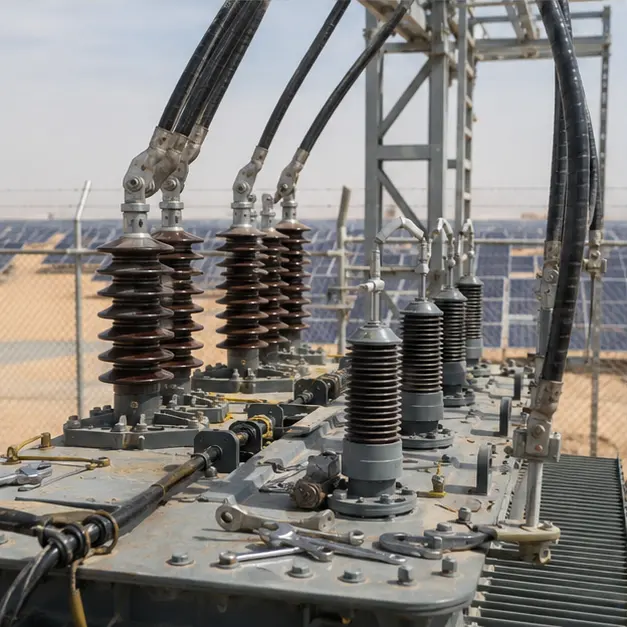
Terminations — High-voltage termination and gantry connection work typical of a 33 kV/13.8 kV solar step-up bay
Termination work is what ultimately decides how reliable the bay proves to be. Bushing surfaces get cleaned and kept clear of conductive dust before anything is connected. Connectors have to match the conductor material — pairing aluminium with copper needs a bimetallic interface, or the joint will corrode and run hot — and every bolted connection is torqued to its specified value and logged. Contact resistance gets measured, never assumed. Connections to the station gantry are designed to allow for thermal expansion as well as wind and short-circuit forces, so flexible connectors go in wherever a rigid conductor would otherwise load up the bushing stem. Arresters are fitted with the shortest earth lead practically possible, since lead inductance adds directly onto the protective level the transformer actually sees.
Completed configuration — Completed configuration of a 33 kV/13.8 kV oil-immersed transformer bay for a utility-scale PV plant
Before energisation, the finished bay is proved as a complete system. Turns ratio, winding resistance, vector group, insulation resistance and, where called for, oil dielectric strength and moisture content are all measured and recorded. Earth grid resistance is measured, and continuity from tank, fence and gantry back to the grid is confirmed. Protection gets tested end-to-end by injection so relay, CT circuit and trip coil are proved together as one chain, and Buchholz, pressure-relief and temperature contacts are functionally checked. Fencing, clearances, signage and access control round out the safety case. Energisation then proceeds in stages, with the unit charged unloaded first before inverter blocks come on progressively while temperatures are watched.
Specification options
For a comparable solar step-up enquiry, Millenium can adjust the voltage ratio and tapping range, offer off-circuit or on-load tap changing, and set capacity, vector group and impedance to match the grid code and the inverter block arrangement. Windings can be copper or aluminium, with insulation and temperature-rise limits set for a high design ambient and extra margin allowed for harmonic loading where needed. Cooling can be specified as ONAN, ONAF or a staged combination with automatic fan control. Bushing creepage can be increased for heavy pollution, and coating class, gasket material and hardware finish selected to suit UV and sand exposure. Accessories on offer include Buchholz and pressure-relief devices, oil and winding temperature indication, oil-level and dehydrating breather monitoring, online monitoring, and communication to the plant SCADA over IEC 61850, Modbus or DNP3.
What we need to quote
Single-line diagram of the plant and the grid connection point
HV and MV voltages, tapping range, tap changer type and required vector group
Transformer capacity and the expected daily PV generation profile
Inverter type and expected harmonic spectrum or K-factor requirement
Grid fault level, required short-circuit withstand and clearing time
Neutral earthing arrangement and the protection philosophy, including differential scheme
Site design ambient temperature range, altitude, wind loading and seismic requirement
Pollution and dust class, and any salinity exposure, for creepage and coating selection
Utility or grid operator specification, grid code and approval requirements
Communication protocol and SCADA points list required
Foundation, oil containment and gantry interface drawings, plus site access and crane availability
Delivery terms, destination port, documentation language and required type and routine test certificates
Quotation
Quote a comparable Saudi Arabia project
Tick what you can already provide — it is added to your message — then send the inquiry. Missing items are not a problem; we will ask.