ISO 9001 · ISO 14001 · ISO 45001 · CE · UDEM · EAC · CQC
🇲🇽 Mexico · Automotive manufacturing
Mexico: 13.8 kV/480 V Substation for an Automotive Components Plant
Reference configuration: 13.8 kV/480 V compact substation with coordinated MV and LV switchgear and bus duct for automotive components manufacturing plant in…
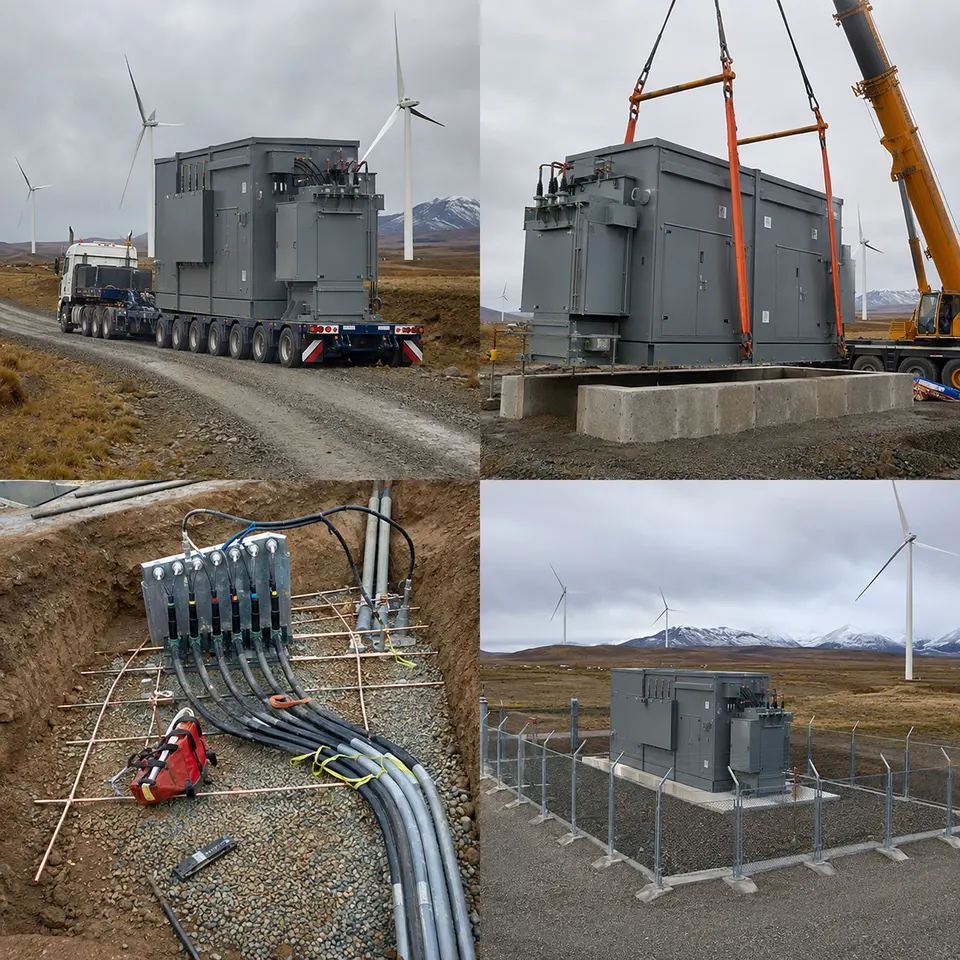
Four-stage sequence typical of a compact substation used for 13.8 kV/480 V factory supply in Mexico
Representative project visualisation. Every image in this set is a representative visualisation of a typical build of this equipment class — none of them is a photograph or documentary record of a completed job, and none stands in for any specific customer, plant, operator, utility, contract, commissioning date, or third-party sign-off. The ratings, quantities and layout shown here are illustrative starting points that would be pinned down against an actual enquiry.
At a glance
Country
Mexico
Location
Monterrey (as stated in the source material)
Application
Automotive components manufacturing plant
System
13.8 kV/480 V compact substation with coordinated MV and LV switchgear and bus duct
Voltage
13.8 kV incoming / 480 V outgoing
Frequency
60 Hz
Standards basis
NOM-001-SEDE (Instalaciones Eléctricas) in the edition current at the time of supply, with NMX-J standards administered through ANCE and CFE's own equipment specifications for anything interfacing with the utility network; ANSI/IEEE C57 series for the transformer, IEEE C37 series for the switchgear, IEEE 519 for harmonic limits at the point of common coupling, IEEE 242 practice for protective device coordination, NFPA 70E and IEEE 1584 practice for arc-flash assessment
Mexico runs an ANSI market on a 60 Hz grid, and both parts of that fact reshape the equipment. Because 480 V is a North American industrial secondary voltage, the LV switchgear, motor control and bus duct all follow ANSI/IEEE and NEMA convention rather than the IEC 400 V norms used elsewhere. At 60 Hz the core runs at a different volts-per-turn for a given flux density, so a transformer built for a 50 Hz market simply does not carry over — core cross-section, losses, sound level and the ratings of magnetics throughout the installation are all affected. Dropping an IEC 50 Hz unit into a Mexican single-line is one of the costlier mistakes possible on a project like this. Wherever the equipment touches the utility network, CFE's own specifications apply on top of the national installation standard, with compliance evidenced through certification to the relevant NMX standards.
The plant's own load profile is the second driver. An automotive components factory brings two difficult load types together at once. Variable-speed drives on presses, conveyors and machine tools inject characteristic harmonic currents, which raise transformer winding eddy losses and can set up resonance with power-factor correction capacitors. Resistance welding causes trouble of a different kind — short, heavy, often single-phase draws that produce voltage flicker and phase unbalance rather than steady distortion. IEEE 519 limits what can be pushed back onto the point of common coupling, but the internal challenge — holding voltage steady enough that welders and drives both run reliably — comes down to transformer impedance, bus duct rating and where correction and filtering equipment sit.
Protection coordination has to tie both problems together: grading from the utility interface through the transformer to the 480 V main and its outgoing feeders must clear a fault quickly enough to keep arc-flash energy under control, while still preserving selectivity so a fault on one production line doesn't take the whole plant down.
System configuration
Item
Description
Specification notes
Compact substation
Outdoor compact or box-type substation housing MV switching, transformer and LV interface
Enclosure IP rating, corrosion category and coating specified for the local climate; foundation, clearances and access arranged for utility and plant maintenance separately
MV switchgear
13.8 kV incoming switching, protection and metering
Metal-enclosed or metal-clad arrangement to IEEE C37 practice; interrupting rating set by the utility fault level; utility metering compartment and sealing arranged to CFE requirements
Transformer
13.8 kV/480 V, 60 Hz, delta primary and earthed star secondary
ANSI/IEEE C57 basis; core and coil designed for 60 Hz; impedance chosen low enough to hold voltage under welding and motor starting yet high enough to keep 480 V fault current within the switchgear rating; K-factor or harmonic loss allowance set against the drive content
LV switchgear and bus duct
480 V main switchboard, feeder sections and bus duct to the plant electrical room
Bus duct continuously rated for the full transformer output with the correct temperature rise and short-circuit bracing; expansion fittings on long runs; ampacity checked at the actual ambient inside the plant
System earthing
Solidly earthed or high-resistance earthed 480 V neutral
High-resistance earthing keeps the plant running through a first earth fault, which suits continuous production, but requires a fault-locating scheme and insulated-neutral discipline; the choice is made against the plant's tolerance for unplanned stoppage
Protection and coordination
MV overcurrent and earth fault, transformer protection, LV main and feeder devices
Time-current grading verified by a coordination study; arc-flash incident energy assessed and labelled; instantaneous and maintenance settings arranged so that work on live equipment is not the default
Power quality
Power-factor correction, detuned reactors or harmonic filtering as required
Correction detuned or filtered where drive content risks resonance; flicker from welding assessed separately from harmonic distortion, since the mitigation is not the same
Metering and monitoring
Utility metering, plant sub-metering, power quality recording
Permanent recording at the main incomer gives the record needed to resolve a power-quality dispute or a production complaint
Communication
Gateway to the plant energy management or SCADA system
Modbus RTU/TCP, DNP3 or IEC 61850 depending on the plant's existing system and points list
Installation sequence
Overview — Four-stage sequence typical of a compact substation used for 13.8 kV/480 V factory supply in Mexico
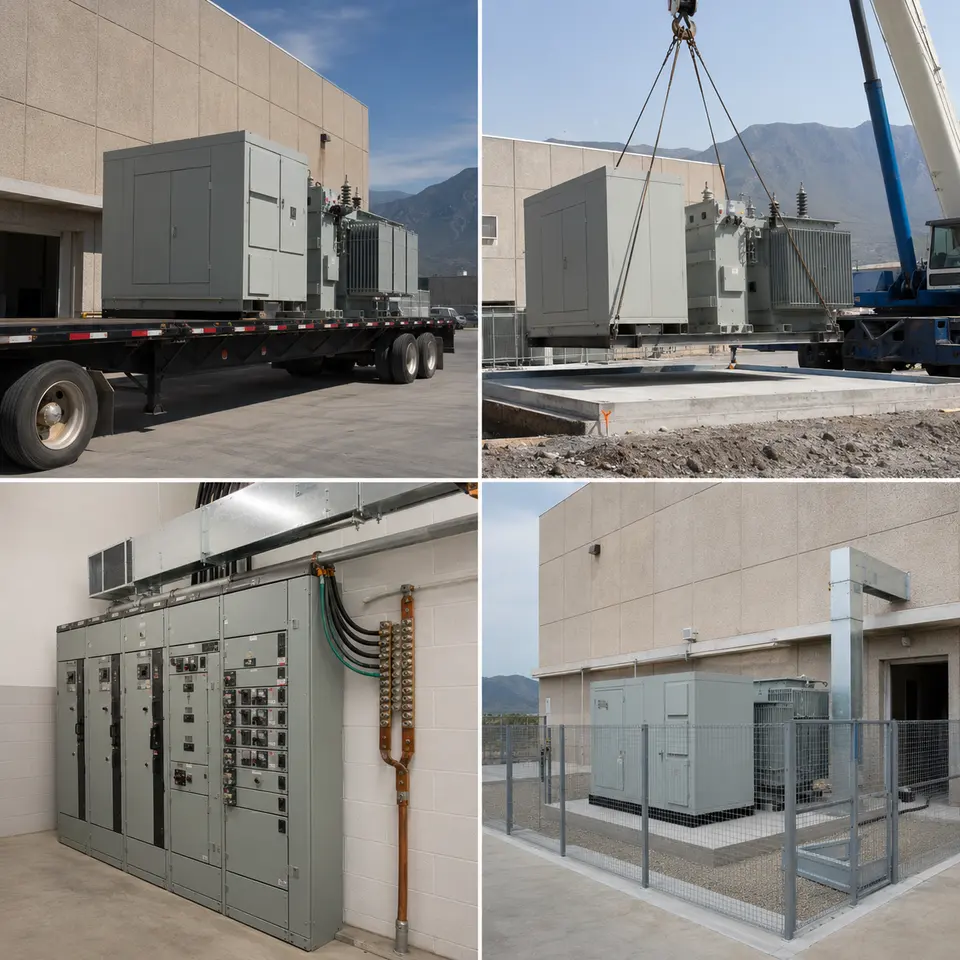
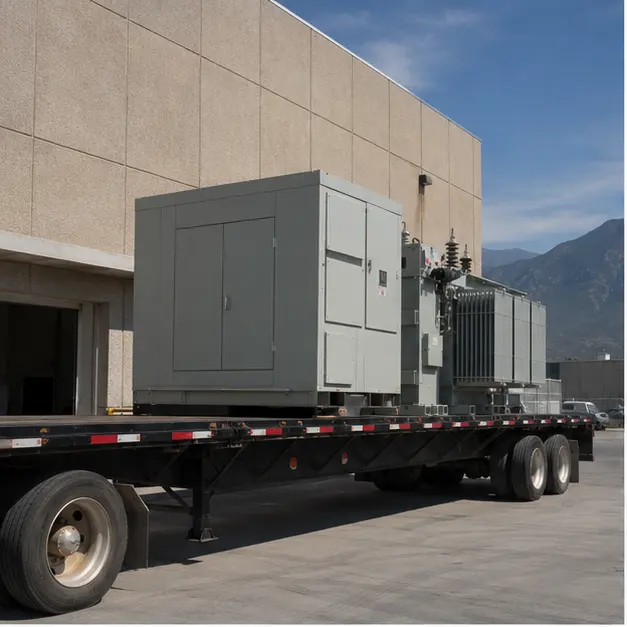
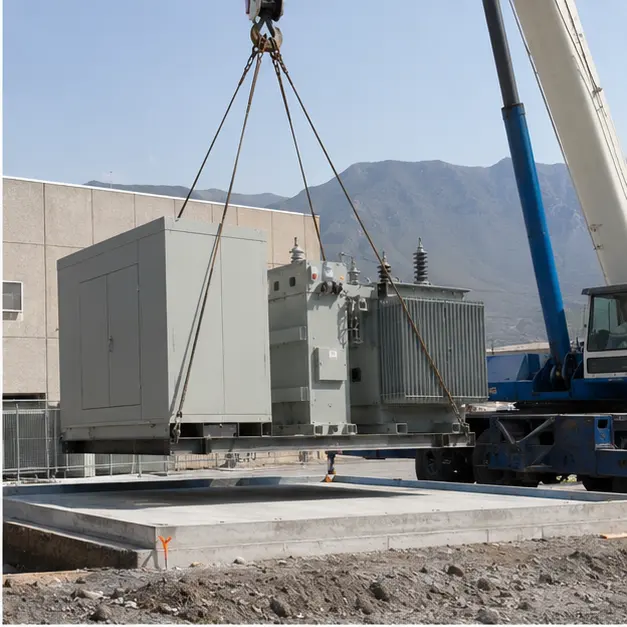
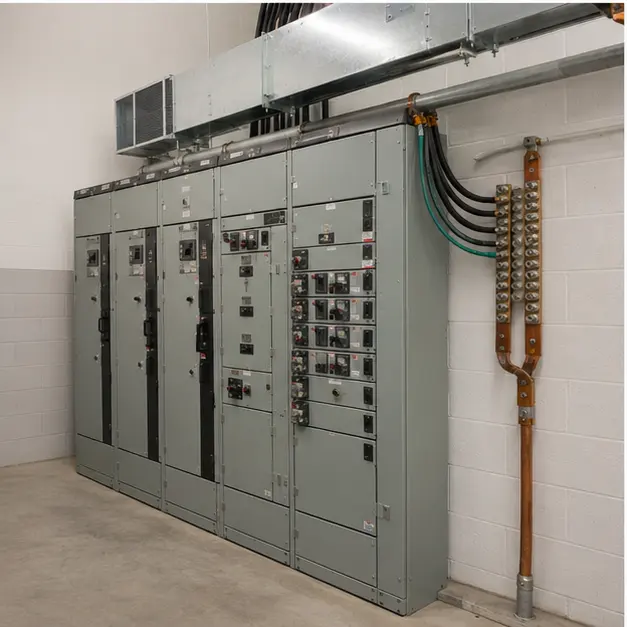
The contact sheet lays out four stages typical of this kind of installation: equipment delivery, crane positioning on the outdoor foundation, indoor switchgear and bus duct connection, and the finished, fenced installation beside the plant electrical room. Sequencing is dictated both by what becomes inaccessible and by what the factory can tolerate. Foundation, ducts, earth grid and drainage are finished and verified before the substation is landed. Bus duct dimensions are taken from the geometry actually built between the outdoor unit and the indoor board, not scaled off a drawing. Any testing requiring open panels happens before the compound is closed up, and connecting production loads is timed around a shutdown window the plant will not want stretched.
Delivery — Delivery of a compact substation of this type to an automotive components plant
Delivery planning is driven by the plant site itself, not just the open road leading to it. Route survey covers axle loading, gradients, gate and yard turning radii, overhead services, and the crane's standing position — often the real constraint on a working factory site. The unit is lashed to prevent lateral movement, since a compact substation is tall for its base and carries its mass low and off-centre where the transformer sits. On arrival it is inspected before being accepted: enclosure checked for transport damage, door and louvre alignment and seal condition verified, internal equipment checked for shifted fixings, and the transformer examined for oil level and gasketed joints or, on a cast-resin unit, for cracking or chipping at the coil ends. Insulation resistance is measured on receipt to set a baseline.
Placement — Crane positioning of a compact substation onto an outdoor foundation, typical of an installation of this type
Setting the unit onto the outdoor foundation is the critical lift. The lift uses designated lugs or corner points with a spreader beam so slings never bear on the enclosure walls, and crane capacity is assessed at working radius with outrigger bearing pressure checked against the yard surface — which in a working factory yard often hides ducts and drainage. Level is confirmed before the unit is set down: an out-of-level enclosure distorts door seals, undermines the ingress rating and throws off alignment with the bus duct flange the indoor run must meet. Clearances to the building, the boundary and vehicle routes are checked against the layout and against whatever access the utility needs to its metering compartment. Anchoring then follows the wind and seismic detail for the location rather than being left as a nominal fixing.
Internal work — Indoor 480 V switchgear and bus duct connection typical of an arrangement of this configuration
Indoor work covers the 480 V switchboard, the bus duct run and the earthing system. Bus duct is set out with its expansion fittings positioned to absorb thermal movement, supported at the required intervals, and aligned so joints are never pulled into place — a strained joint runs hot. Joint bolts are tightened to the specified torque using the manufacturer's indicating method, with each joint marked afterward, because contact resistance is what turns a properly rated connection into a failure point. Phase sequence and phase identification are checked through the entire run before it is closed up. The switchboard is bonded to the plant earth grid with a conductor sized for the prospective earth-fault current and clearing time, and the bus duct enclosure is bonded continuously across every joint. Insulation resistance is measured on the finished run, and interlocks are proved by actually operating them rather than by visual check alone.
Completed configuration — Completed configuration of a 13.8 kV/480 V compact substation serving an automotive components plant
The finished configuration shows the compact substation fenced and labelled outside the plant, feeding the indoor 480 V board through bus duct. Ahead of energisation the installation is proved end to end: transformer ratio and vector group checked on every tap, winding resistance and insulation resistance recorded, earth continuity confirmed from every enclosure back to the grid, and protection proved by injection so relay, CT circuit and trip device are all shown to work together. Coordination and arc-flash study results are checked against the settings actually applied, and labels are fitted to match. Energisation proceeds in stages — transformer charged unloaded, then the 480 V board, then production loads brought on line by line — with voltage, unbalance and distortion recorded during the first welding and drive operation, since those are exactly the conditions the impedance and power-quality design were chosen to handle.
Specification options
For a comparable factory enquiry, Millenium can engineer the voltage ratio and tapping range, capacity, vector group and impedance against the plant's motor and welding duty, at 60 Hz, in copper or aluminium windings. The transformer is available as cast-resin dry-type for indoor placement or oil-immersed with containment for outdoor use, with insulation class, temperature-rise limits and a harmonic loss allowance set against the drive content. MV switching can be metal-enclosed or metal-clad with the required interrupting rating and a utility metering compartment. LV switchboards can be built to the required short-circuit rating, bracing and access arrangement, with bus duct rated and braced for the transformer output. Enclosures can be specified for IP rating, corrosion category and coating class. Power-factor correction can be plain, detuned or filtered, and monitoring can extend to permanent power quality recording reported over Modbus, DNP3 or IEC 61850.
What we need to quote
Single-line diagram of the utility interface, the substation and the 480 V distribution
Incoming 13.8 kV details, tapping range and step size, and the required vector group
Transformer capacity, plant load profile, load factor and any planned production expansion
Motor schedule with the largest motor and its starting method, and the variable-speed drive inventory with expected harmonic spectrum
Welding load description — type, duty cycle, single- or three-phase — for flicker and unbalance assessment
Utility short-circuit level at the point of common coupling and the applicable CFE specification and metering requirements
480 V system earthing decision — solidly earthed or high-resistance — and the plant's tolerance for a first-fault stoppage
Protection philosophy, existing coordination study, and arc-flash assessment and labelling requirements
Power-factor target, any existing correction equipment, and measured power quality data if available
Room layout, bus duct route with lengths and offsets, headroom, and the indoor ambient temperature for ampacity
Site ambient temperature range, altitude, dust exposure, corrosion category and wind and seismic design data
Communication protocol, energy management system points list, available shutdown window and delivery terms
Quotation
Quote a comparable Mexico project
Tick what you can already provide — it is added to your message — then send the inquiry. Missing items are not a problem; we will ask.