ISO 9001 · ISO 14001 · ISO 45001 · CE · UDEM · EAC · CQC
🇧🇷 Brazil · Solar
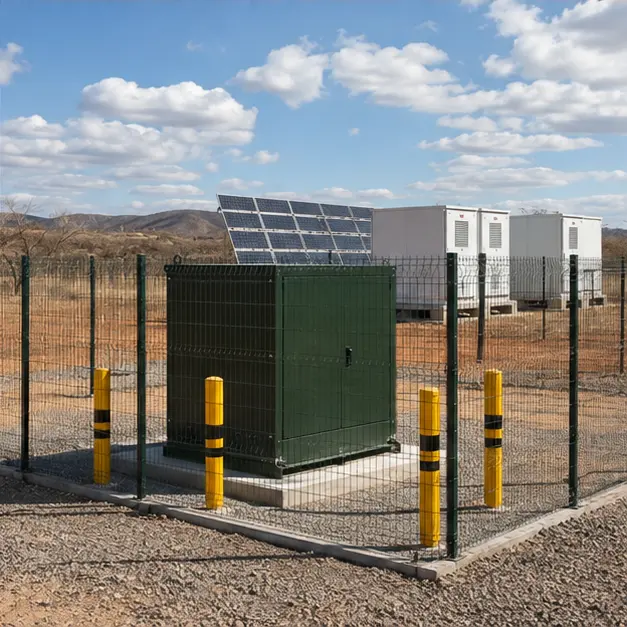
Brazil: 34.5 kV/480 V Solar Pad-Mounted Transformer
Reference configuration: 34.5 kV/480 V three-phase pad-mounted transformer, dead-front for utility photovoltaic power plant in Brazil — 34.5 kV collector /…
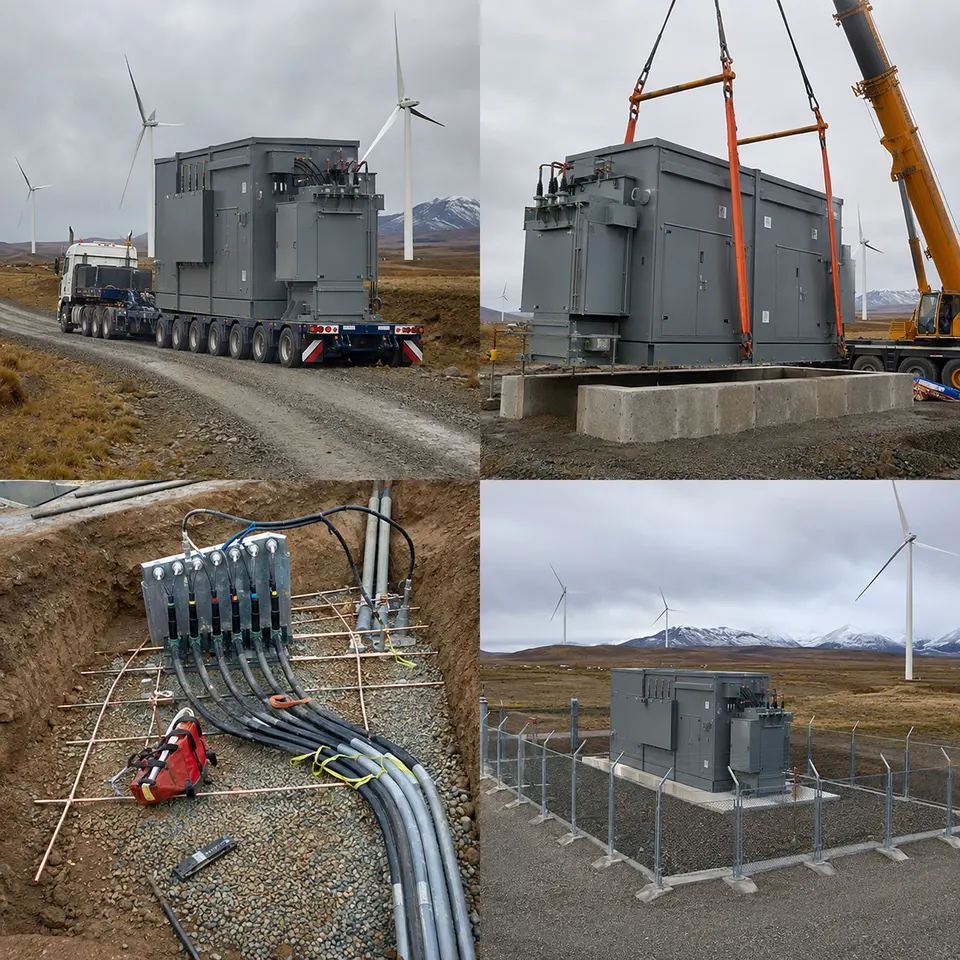
Four-stage build sequence typical of a pad-mounted transformer on 34.5 kV solar collector systems in Brazil
Representative project visualisation. Representative visualisation only. Every image in this set is a representative rendering of a typical build for this equipment class — not a photograph, and not documentary proof that a specific project was completed. No particular customer, plant, developer, concessionária, contract, commissioning date or third-party sign-off is being represented here. The ratings, quantities and layout shown are illustrative examples that would be pinned down against an actual enquiry.
At a glance
Country
Brazil
Location
Bahia (as stated in the source material)
Application
Utility photovoltaic power plant
System
34.5 kV/480 V three-phase pad-mounted transformer, dead-front
Voltage
34.5 kV collector / 480 V inverter side
Frequency
60 Hz
Standards basis
ABNT NBR 5356 series (power transformers, aligned with IEC 60076), ABNT NBR 5440 and ABNT NBR 14039 for MV installations, IEEE C57.12.34 for three-phase pad-mounted compartmental construction, IEEE 386 for separable insulated connectors, ANEEL PRODIST for distributed connection requirements
A Brazilian utility-scale PV plant collects its power at 34.5 kV, and that one number shapes everything else about the design. It is high enough to carry plant-scale power over kilometres of buried collector cable without excessive loss, and it happens to be the standard Brazilian rural and industrial distribution class, so the equipment, cable, elbows and protection all come from a mature domestic catalogue rather than a bespoke build.
On the inverter side, 480 V is a deliberate compromise — high enough to keep inverter output current and cable size reasonable, low enough to stay inside ordinary LV switchgear and cable practice. The transformer sitting between the two therefore steps up rather than down, and spends its working life driven by an inverter rather than serving a conventional load. That reshapes the spec in several ways. Harmonic current from the inverter adds eddy and stray losses, so a K-factor or harmonic-loading assessment belongs in the sizing calculation from the start. The duty cycle is heavily cyclic — full output at midday, nothing at night — which makes no-load loss add up economically across a plant's entire transformer fleet, and makes thermal cycling, rather than steady heating, the real ageing mechanism. Ratio and vector group must align with the inverter manufacturer's earthing and grounding-transformer requirements, since the step-up transformer is usually what earths the PV block on the MV side.
The dead-front pad-mounted format answers the physical side of the problem. A PV site is large, sits along a public boundary, and is largely unattended. A tamper-resistant, sealed, ground-level enclosure with every live part behind an insulated interface removes exposed terminals from the site altogether, needs no elevated structure, and can be delivered and set in a single lift — while also suiting the loop-feed collector topology used to string blocks together.
System configuration
Item
Description
Specification notes
Transformer
34.5 kV/480 V three-phase pad-mounted step-up unit, oil-immersed, hermetically sealed
Built to ABNT NBR 5356; vector group and MV earthing arrangement matched to the inverter's requirement; impedance chosen against inverter fault contribution and collector voltage regulation
Separate HV and LV compartments with a defined opening sequence; ISO 12944 coating category and paint system selected for solar radiation and site exposure
HV interface
Loadbreak or deadbreak separable connectors on bushing wells, loop-feed or radial
IEEE 386 elbows with capacitive test points and parking stands; loop-feed arrangement allows a block to be isolated without dropping the collector run
HV protection
Bayonet and backup current-limiting fuses, or an internal switch with fusing
Fuse coordination set against inverter transformer inrush and the upstream collector protection
LV interface
480 V spade or bar terminals in the LV compartment, multiple inverter cable ways
Terminal count and cable entry sized to the inverter cable arrangement; non-magnetic gland plates used with single-core cables
Surge protection
MV surge arresters, elbow-type or bracket-mounted
Rating and energy class selected against the collector system earthing and local lightning density, which runs high across much of Brazil
Thermal design
Radiators or corrugated tank walls, sealed oil system with no conservator
Temperature rise limits set for design ambient and the cyclic PV duty; harmonic loading from inverters factored into the loss calculation
Earthing
Tank, enclosure, arrester and cable screen bonding to the site earth grid
Conductor sized for prospective earth-fault current and clearing time; step and touch potential assessed for a publicly accessible pad
Monitoring
Oil temperature, level and pressure indication, optional contacts to the plant SCADA
Alarm and trip contacts wired to the plant control system wherever equipment of this kind is remotely supervised
Installation sequence
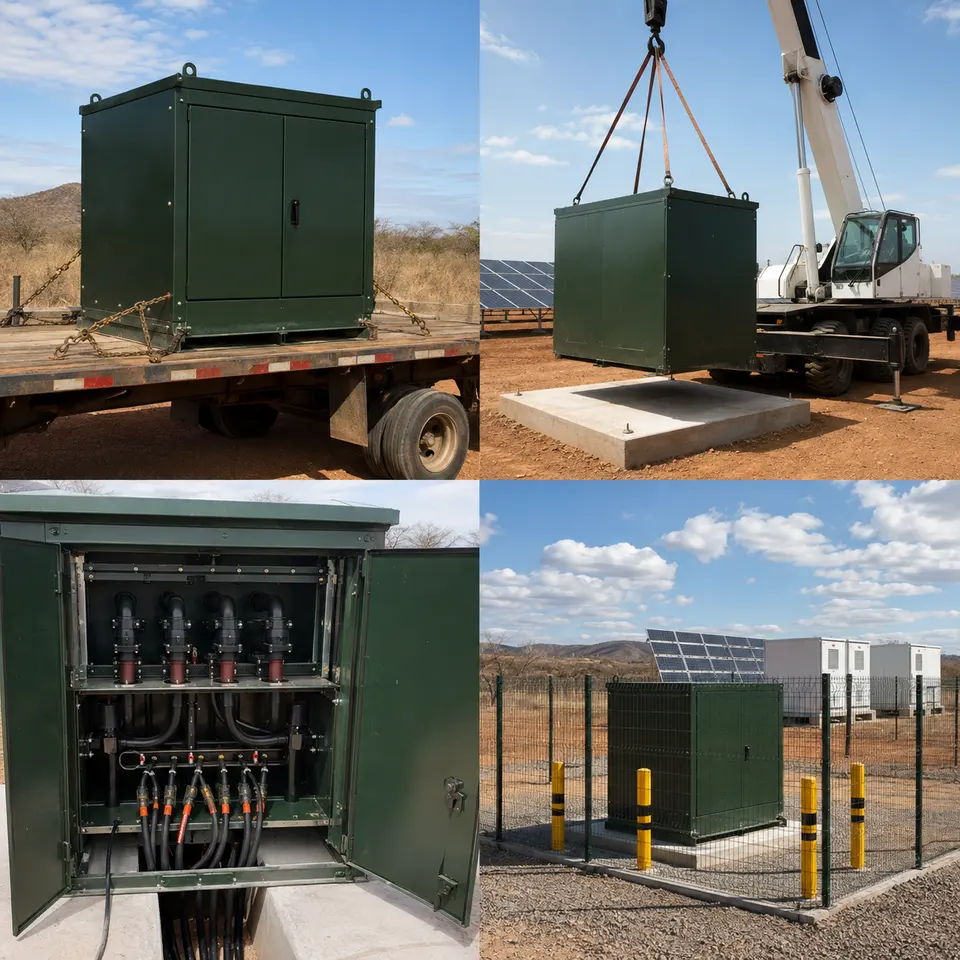
Overview — Four-stage build sequence typical of a pad-mounted transformer on 34.5 kV solar collector systems in Brazil
This contact sheet lays out the four stages a project of this kind moves through: delivery to the block position, the crane lift onto the pad, dead-front cable connection, and the finished, fenced installation. The sequence is governed by the concrete. The pad, its cable stub-ups, conduit entries and earth grid connections all have to be finished, cured and surveyed before the transformer arrives, because once it lands nothing underneath it can be reached again. Cable is pulled and left long, and only terminated once the transformer is in position and its bushing locations are known. Any testing that needs the compartments open is finished before the enclosure is closed, locked and the block handed to commissioning.
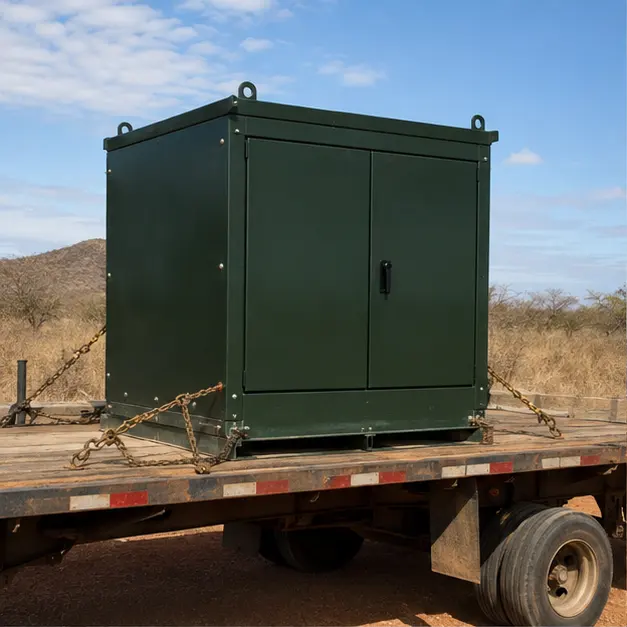
Delivery — Delivery of a pad-mounted transformer of this kind to a photovoltaic plant block position
Getting a unit into a PV block is a slow, off-road transport exercise. Internal plant roads are typically unsealed, and a pad-mounted transformer carries its weight low but concentrated, so lashing has to stop sideways movement rather than simply hold the unit down against gravity. After a long haul, it is worth reading any impact recorder fitted before unloading. Receiving inspection covers transport damage, paint condition — a scratched coating on a Bahia site becomes a corrosion point quickly — oil level in the sight glass, the pressure-vacuum gauge reading, bushing and bushing-well condition, and confirming the elbows, parking stands and arresters listed on the packing note are all present. Any positive or negative internal pressure is logged before the tank is opened.
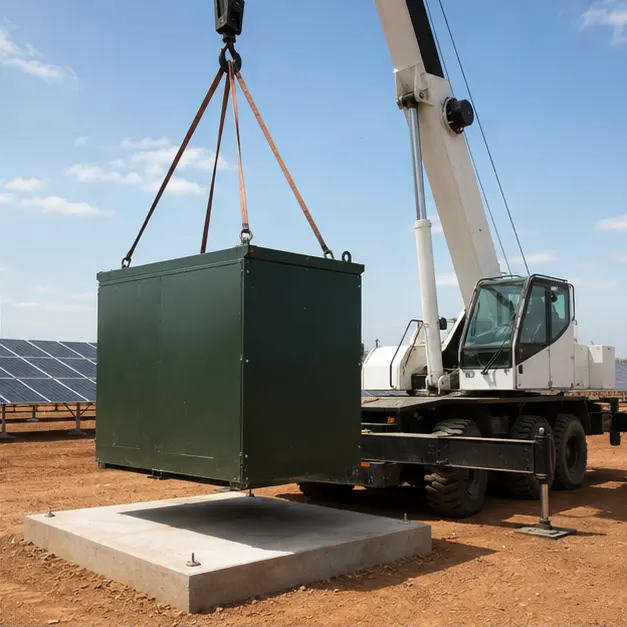
Placement — Crane lift onto a concrete pad, characteristic of a solar installation of this type
The lift itself is quick, but there is little room for error. The pad is confirmed level and its cable window checked against the transformer footprint before lifting begins, because a unit set even slightly out of level will not shed water from its roof and will load its gasketed joints unevenly. Lifting uses the four designated lugs with a spreader bar so slings never bear on radiators, bushings or the cabinet. Crane capacity is assessed at working radius, with outrigger bearing pressure checked against the ground actually present — soft ground next to a freshly poured pad is a frequent cause of an aborted lift. The unit is set down clear of the stub-up cables, oriented so the HV and LV compartments face the intended access side, and anchored to the pad.
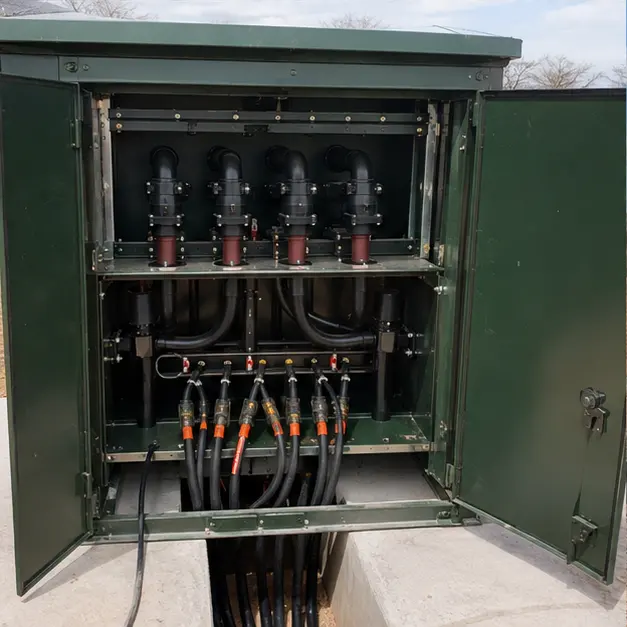
Cable work — Dead-front separable connector and earthing work in a pad-mounted arrangement of this type
The dead-front interface is the whole reason this format gets used, and it is also where workmanship risk concentrates. Cable is cut to length while respecting the bending radius into the compartment — force a 34.5 kV cable around too tight a radius and it damages the insulation shield without failing immediately. Elbow preparation follows the same discipline as any MV termination: correct cut-back, removal of the semiconducting layer, cleanliness, and the specified lubricant, with the connector fully seated so its capacitive test point reads correctly. Elbows are only operated with a hotstick, and only within their loadbreak rating; deadbreak connectors are never switched under load at all. Cable screens and arrester earths bond to the site grid through a conductor rated for the earth-fault duty, and LV terminals are torqued to value and marked.
Completed configuration — Finished configuration of a 34.5 kV/480 V pad-mounted transformer serving a photovoltaic plant
Before energisation the block is proved as a complete chain. Turns ratio is measured on every tap and the vector group verified, because a wrong group on one block of a multi-block PV plant will not show up until the inverters try to synchronise. Winding and insulation resistance are recorded, oil condition and dielectric strength are confirmed, and earth continuity is proved from the tank, cabinet, arrester bases and cable screens back to the site grid, with grid resistance logged. Fuses are checked for correct rating, protection grading against the collector feeder is confirmed, and the enclosure is closed and locked. Energisation is staged — the collector feeder first, then the transformer charged unloaded from the MV side, then inverters brought online progressively as irradiance allows.
Specification options
For a comparable PV enquiry, Millenium can configure capacity, primary and secondary voltage, tapping range, vector group and impedance to suit the inverter manufacturer's requirement and the collector system study, with copper or aluminium windings. Transformers can be supplied hermetically sealed or with a conservator, filled with mineral oil or a less-flammable ester fluid where fire separation distances are tight, with temperature rise and insulation class set for design ambient and the cyclic PV duty. Dual-secondary and split-winding arrangements are available where two inverters share one unit. Enclosures can be specified for coating system and corrosion category, tamper-resistant hardware, loop-feed or radial HV interface, loadbreak or deadbreak elbows, bayonet plus backup fusing or an internal switch, and integrated surge arresters. Monitoring can extend to oil temperature, level and pressure contacts, winding temperature indication, and reporting over Modbus, IEC 61850 or DNP3.
What we need to quote
Single-line diagram of the collector system showing the block arrangement and loop-feed topology
Transformer capacity per block and the number of units required
Primary and secondary voltage, tapping range, required vector group and MV earthing arrangement
Inverter make, model, output arrangement and its transformer requirements, including harmonic content
Collector system fault level, protection philosophy and upstream feeder relay settings
Site ambient temperature range, solar radiation exposure, altitude, dust and lightning density
Distribuidora or concessionária connection specification and any applicable ANEEL PRODIST requirements
HV interface type — loadbreak or deadbreak elbows, bushing well arrangement, parking stands
LV terminal arrangement, cable size and number of cable ways per phase
Enclosure coating and corrosion class, tamper-resistant hardware requirement, and pad detail
Monitoring contacts, communication protocol and the plant SCADA points list
Site access route, permissible axle loading, available crane capacity and delivery terms
Quotation
Quote a comparable Brazil project
Tick what you can already provide — it is added to your message — then send the inquiry. Missing items are not a problem; we will ask.